
Best filament dryer
The best filament dryers in 2026
Dryer picks split by temperature range and capacity, because a 70 C unit and a 110 C unit are different products for different materials.
Wet filament imitates six other faults convincingly. Drying is the cheapest thing you can do to a print, and the one most owners try last.
By Michael W. · Published October 5, 2026
Here is the pattern. Prints start stringing. You tune retraction. It helps a bit. You drop the temperature. The layers get weaker. You clean the nozzle, buy a new nozzle, consider a new printer. Then someone mentions drying the spool, you leave it in a box for six hours, and the problem disappears.
That sequence is so common it is practically a rite of passage, and it is why this hub exists. Moisture is the most-misdiagnosed fault in 3D printing because its symptoms belong to other things.
Three signs, and the first is nearly conclusive. Popping or hissing from the nozzle during a print is steam, and steam means water. Filament that snaps when you bend it instead of flexing has usually been hydrolyzed, which is a chemical change rather than simple dampness. And stringing that gets worse through a long print rather than being constant from the first layer points at the spool heating up and releasing moisture, not at a slicer setting.
Rough or furry surfaces and weak, brittle finished parts are the slower-burning versions of the same thing. The complete list and what each one rules out is on wet filament symptoms.
Not all filament is equally hygroscopic, and the gap is wide enough to change what you should buy.
That last point decides the purchase. A dryer that tops out around 70 C covers PLA, PETG and TPU, which is most hobby printing. Nylon and polycarbonate want substantially more heat, which is a different and more expensive class of unit — the dryer roundup splits them for exactly that reason, and the best dryer under $100 covers the budget bracket where every unit shares that same ceiling.
A single-spool dryer is fine if you print one color at a time. The moment you run four-color jobs, drying one spool while three sit absorbing moisture is close to pointless, and a four-spool unit is the only capacity that matches the workflow — the SUNLU S4 review is the four-spool box examined in detail, including the temperature ceiling that comes with it. If you own an AMS, drying inside the unit you print from — an AMS 2 Pro or an AMS HT — closes the gap between drying and printing entirely, which is a real advantage over any standalone box.
Printing while drying is the capability worth paying for if you print anything seriously hygroscopic. Everything else is a convenience.
You can dry PLA and PETG in a kitchen oven, and if you are not sure moisture is your problem it is the right first test. The rules are strict — well below the glass transition temperature, oven thermostats lie by a wide margin, and a convection setting is much safer than a conventional one — and getting them wrong turns a spool into a fused brick. The drying guide covers the oven method, the food-dehydrator method, drying on the print bed, and why each has limits. Then is a dryer worth it answers the purchase honestly, including the case where it is not.
It will not fix a clog caused by debris, a first layer that will not stick because the plate is contaminated, layer shifting, or any mechanical fault. If drying a spool does not change anything, stop drying and go to print quality triage, which sorts symptoms by cause instead of by hope.
Buying: the roundup. Diagnosing: wet filament symptoms. Working out what your printer can even run: filament compatibility.
Best filament dryer
Dryer picks split by temperature range and capacity, because a 70 C unit and a 110 C unit are different products for different materials.
Best dryer for TPU
Why TPU needs a dryer more than any other common filament, and which unit to buy when you want to print straight out of it.
Best dryer for nylon
Nylon and PA6-CF need temperatures most dryers cannot reach - which units are cited as going high enough, and the one you may already own.

Best dryer for PLA
PLA's published oven setting is 50 C - the lowest in the range. A controlled low temperature and sealed storage beat a high ceiling every time.

Best dryer under $100
Three dryers under the line, all in the 70 C class. Capacity and feed-through are what separate them - and the one material group no unit at this price can serve.
What high-flow PETG changes, when the speed is real and when it is not, and why both variants need the same drying either way.

How per-spool sealed boxes differ from four-spool dryers, the humidity figure that matters, and where the modular approach stops scaling.
When capacity matters more than temperature, what long heat-up cycles mean day to day, and the cheaper hybrid of one dryer plus sealed tubs.
What the reabsorption gap costs per material, which units let you print from them, and when closing the gap is worth paying for.
#ad We earn a commission · price as of November 20, 2026
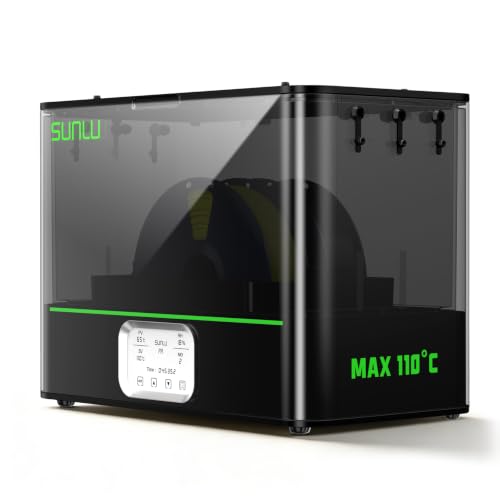
The only 110 C unit in this site's registry. Published range, capacity, timer and heat-up figures - plus the two specs the maker and the retailer disagree on.
Four 1 kg spools at a published 70 C, with filament fed out to up to four printers while it dries. The specs, the two figures retailers disagree on, and who should skip it.
Four drying methods compared, the temperature each material wants, and the one method that does not work despite being widely suggested.
Who a dryer genuinely pays for, who should buy sealed storage instead, and the free test that settles it before you spend.
Which AMS units actually dry, what that gets you over a standalone dryer, and the material ceiling that still applies.
#ad We earn a commission · price as of November 20, 2026
The three near-conclusive signs of wet filament, the ambiguous ones, and the free test that settles it in one print.

A per-machine compatibility table, the three things that actually gate material choice, and which of them you can buy your way past.
Bambu's published oven settings run 50 C for PLA to 80 C for ABS, ASA, PA6-CF and PC - but they specify a forced-air oven, which a kitchen oven is not.
Published heatbed figures are 60-70 C for PLA up to 100 C for PC. The P1S bed tops out at 100 C and an A1 mini at 80 C, which decides what each machine can dry.
#ad We earn a commission · price as of November 20, 2026
PLA, PETG and TPU are the A-series' home ground. ABS and ASA fight the open frame, and the A1 mini's 80 C bed closes off more than the A1's 100 C one.
PA6-CF fits at 260-300 C against the P1S's 300 C ceiling. PPS-CF needs 310-340 C and does not. PPA-CF is listed for the P1S with an enclosure and a hardened nozzle.
Listen for popping or hissing from the nozzle during a print - that is steam, and it is close to conclusive. Then try bending a length of filament: if it snaps rather than flexing, it has absorbed moisture. Stringing that worsens through a long print, rather than being constant from the first layer, is the third sign.
Yes for PLA and PETG, with care. Stay well below the material's glass transition temperature, use convection rather than conventional heat if you have it, and do not trust the dial - domestic oven thermostats are often out by a wide margin, and overshooting fuses the spool into a solid block. A dedicated dryer or a food dehydrator holds temperature far more accurately.
If you print PETG, TPU, nylon or anything carbon-filled, yes - it pays for itself in filament you stop throwing away. If you print only PLA in a dry room, probably not, and a sealed box with desiccant is the better spend. The clearest case for a dryer is a humid climate, where even PLA degrades on an open shelf.
Material-dependent, and the ceiling matters more than the exact number. PLA, PETG and TPU are served by dryers topping out around 70 C. Nylon, polycarbonate and PA-CF need substantially more heat, which is why high-temperature units reaching around 110 C exist as a separate class. Always stay below the material's glass transition temperature.
For most materials, yes, and it does it better, because the spool you dry is the spool you print from - there is no window where a dried spool sits reabsorbing moisture while a long print runs. For nylon and polycarbonate you want higher temperatures than a standard-temperature unit provides, which is where the AMS HT or a dedicated high-temperature dryer comes in.